Machine Vision and Automation Solutions for Industrial Projects
Discover how Valley International Supply offers top-tier machine vision, identification, and automated inspection solutions for industrial automation.
Valley International Supply is dedicated to providing high-quality industrial automation solutions, including machine vision, identification, and automated inspection systems. These technologies are crucial for enhancing efficiency, accuracy, and productivity in manufacturing operations. Whether you need to improve quality control, streamline production processes, or ensure compliance with industry standards, our solutions are designed to meet your specific needs.
Why Choose Machine Vision and Automation Solutions?
Machine vision and automation solutions offer numerous benefits for industrial projects:
- Improved Quality Control: Automated inspection systems can detect defects and inconsistencies with high precision, reducing the likelihood of faulty products reaching the market.
- Increased Efficiency: By automating repetitive tasks, machine vision systems free up human workers to focus on more complex and value-added activities.
- Enhanced Accuracy: Machine vision technology provides consistent and reliable results, minimizing human error and ensuring uniform product quality.
- Cost Savings: Automated inspection and identification processes can reduce labor costs and improve overall operational efficiency.
Key Components of Machine Vision Systems
Machine vision systems typically include the following components:
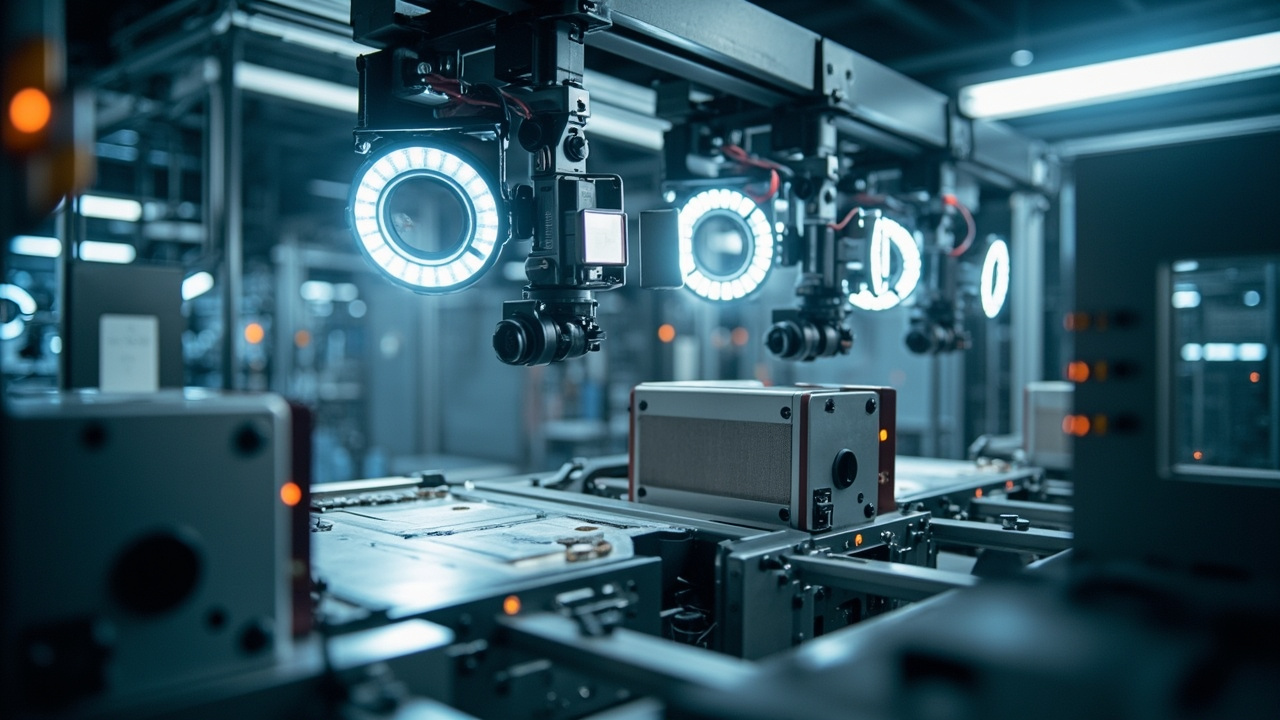
- Cameras: High-resolution cameras capture images of the products or processes being inspected.
- Lighting: Proper lighting is essential for ensuring clear and accurate image capture.
- Software: Advanced software algorithms analyze the captured images to identify defects, measure dimensions, and perform other inspection tasks.
- Processing Units: Powerful processing units handle the computational demands of image analysis and data processing.
Applications of Machine Vision and Automation
Machine vision and automation solutions are used across various industries and applications, including:
- Quality Inspection: Detecting defects in manufactured products, such as cracks, scratches, or misalignments.
- Identification and Tracking: Reading barcodes, QR codes, and other identifiers to track products through the supply chain.
- Assembly Verification: Ensuring that components are correctly assembled and positioned.
- Measurement and Gauging: Accurately measuring dimensions and tolerances to ensure product conformity.
Leading Brands in Machine Vision and Automation
Valley International Supply represents some of the world’s leading manufacturers in machine vision and automation, including:
- STEINEL: Known for their innovative sensor technology and machine vision solutions.
- NOSHOK: Providing precision measurement and control instruments.
- DESCO: Offering a range of industrial automation and control solutions.
- NORGREN: Specializing in pneumatic and fluid control systems.
- FASTEST: Providing high-speed inspection and sorting solutions.
- EATON: Known for their comprehensive range of electrical and industrial automation products.
- SIEMENS: Offering advanced automation and digitalization solutions.
How to Choose the Right Machine Vision Solution
Selecting the right machine vision solution involves considering several factors:
- Application Requirements: Understand the specific needs of your application, such as the type of defects to be detected or the dimensions to be measured.
- Environmental Conditions: Consider the lighting, temperature, and other environmental factors that may affect image capture and analysis.
- Integration Capabilities: Ensure that the machine vision system can be easily integrated with your existing production lines and control systems.
- Scalability: Choose a solution that can scale with your business needs, accommodating future growth and changes.
Next Steps
To learn more about how Valley International Supply can help you implement machine vision and automation solutions for your industrial projects, contact our team of technical experts. We offer personalized service and tailored engineering recommendations to ensure that you get the best possible results.
Frequently Asked Questions
What are the main benefits of using machine vision in industrial automation?
Machine vision offers several benefits, including improved quality control, increased efficiency, enhanced accuracy, and cost savings. By automating inspection and identification processes, machine vision systems can detect defects, track products, and ensure consistent product quality.
How do I choose the right machine vision system for my application?
Choosing the right machine vision system involves considering your specific application requirements, environmental conditions, integration capabilities, and scalability. Our team of experts can help you evaluate these factors and recommend the best solution for your needs.
Can machine vision systems be integrated with existing production lines?
Yes, machine vision systems can be integrated with existing production lines and control systems. Our solutions are designed to be flexible and scalable, ensuring seamless integration and minimal disruption to your operations.
What types of defects can machine vision systems detect?
Machine vision systems can detect a wide range of defects, including cracks, scratches, misalignments, and dimensional inconsistencies. The specific types of defects that can be detected depend on the application and the capabilities of the machine vision system.
How do machine vision systems improve quality control?
Machine vision systems improve quality control by providing consistent and reliable inspection results. They can detect defects and inconsistencies with high precision, reducing the likelihood of faulty products reaching the market and ensuring uniform product quality.
What industries benefit from machine vision and automation solutions?
Machine vision and automation solutions are used across various industries, including manufacturing, automotive, electronics, pharmaceuticals, and food and beverage. Any industry that requires precise inspection, identification, and tracking can benefit from these technologies.
Manufacturers & sources referenced
This article references products from the following manufacturers. Learn more on their official sites:
About Valley International Supply
Valley International Supply is a distributor and OEM manufacturer representative of industrial automation equipment, serving manufacturers across the United States and Mexico for over 30 years. We supply PLCs, drives, HMIs, sensors, pneumatics, safety systems and connectivity components, backed by engineering selection assistance and technical support. Contact us at inquiry@valleyintlsupply.com or +1 (956) 338-0631.